UNCONDITIONAL QUALITY
We aim for the highest standards at every stage of production and guarantee sustainable excellence with our global quality certificates.
OUR QUALITY POLICY
Customer Focus
It is our core principle to meet our customers' expectations at the highest level and ensure continuous satisfaction.
Continuous Improvement
We continuously analyze and modernize our processes with a focus on efficiency and quality.
Food Safety
We do not compromise on global hygiene and safety standards in food-contact packaging.
QUALITY CONTROL PROCESSES
Raw Material Acceptance
All paper and ink raw materials pass laboratory tests during initial quality control processes.
In-Process Control
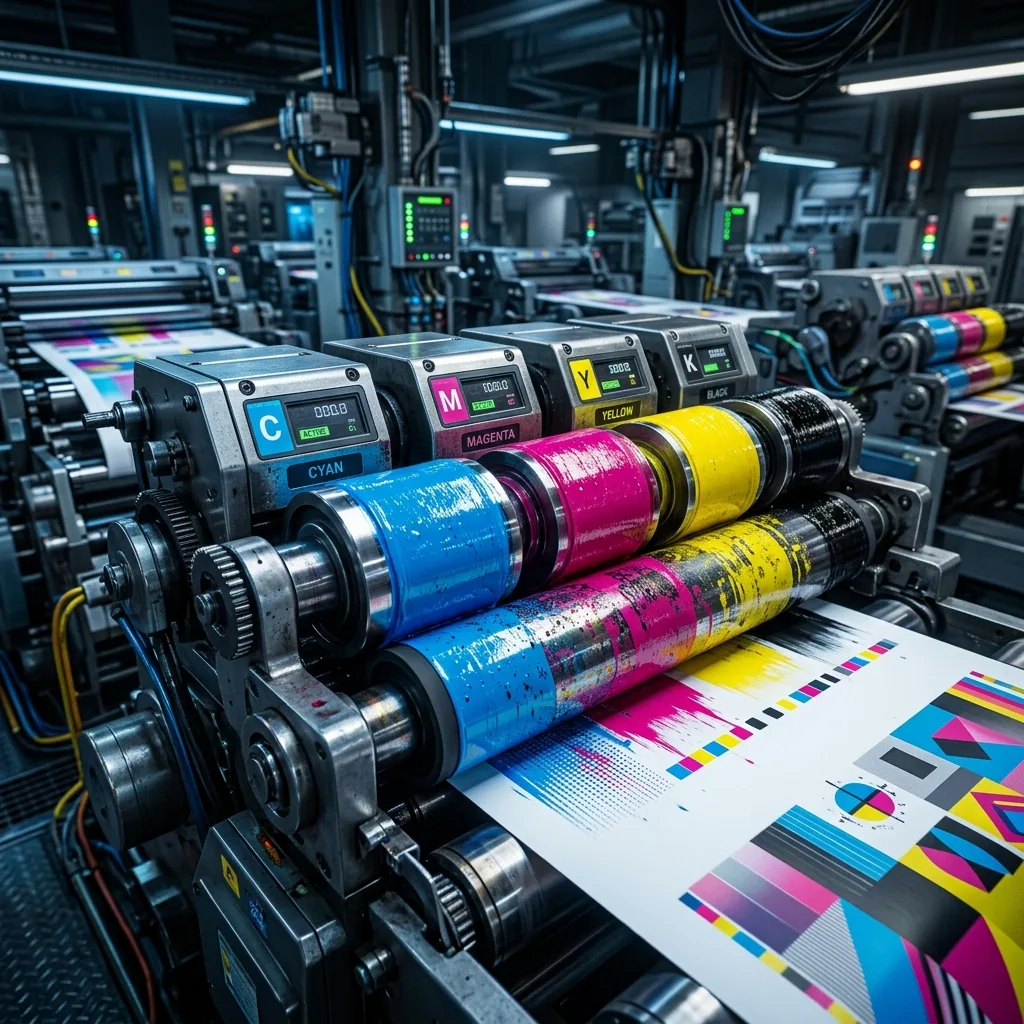
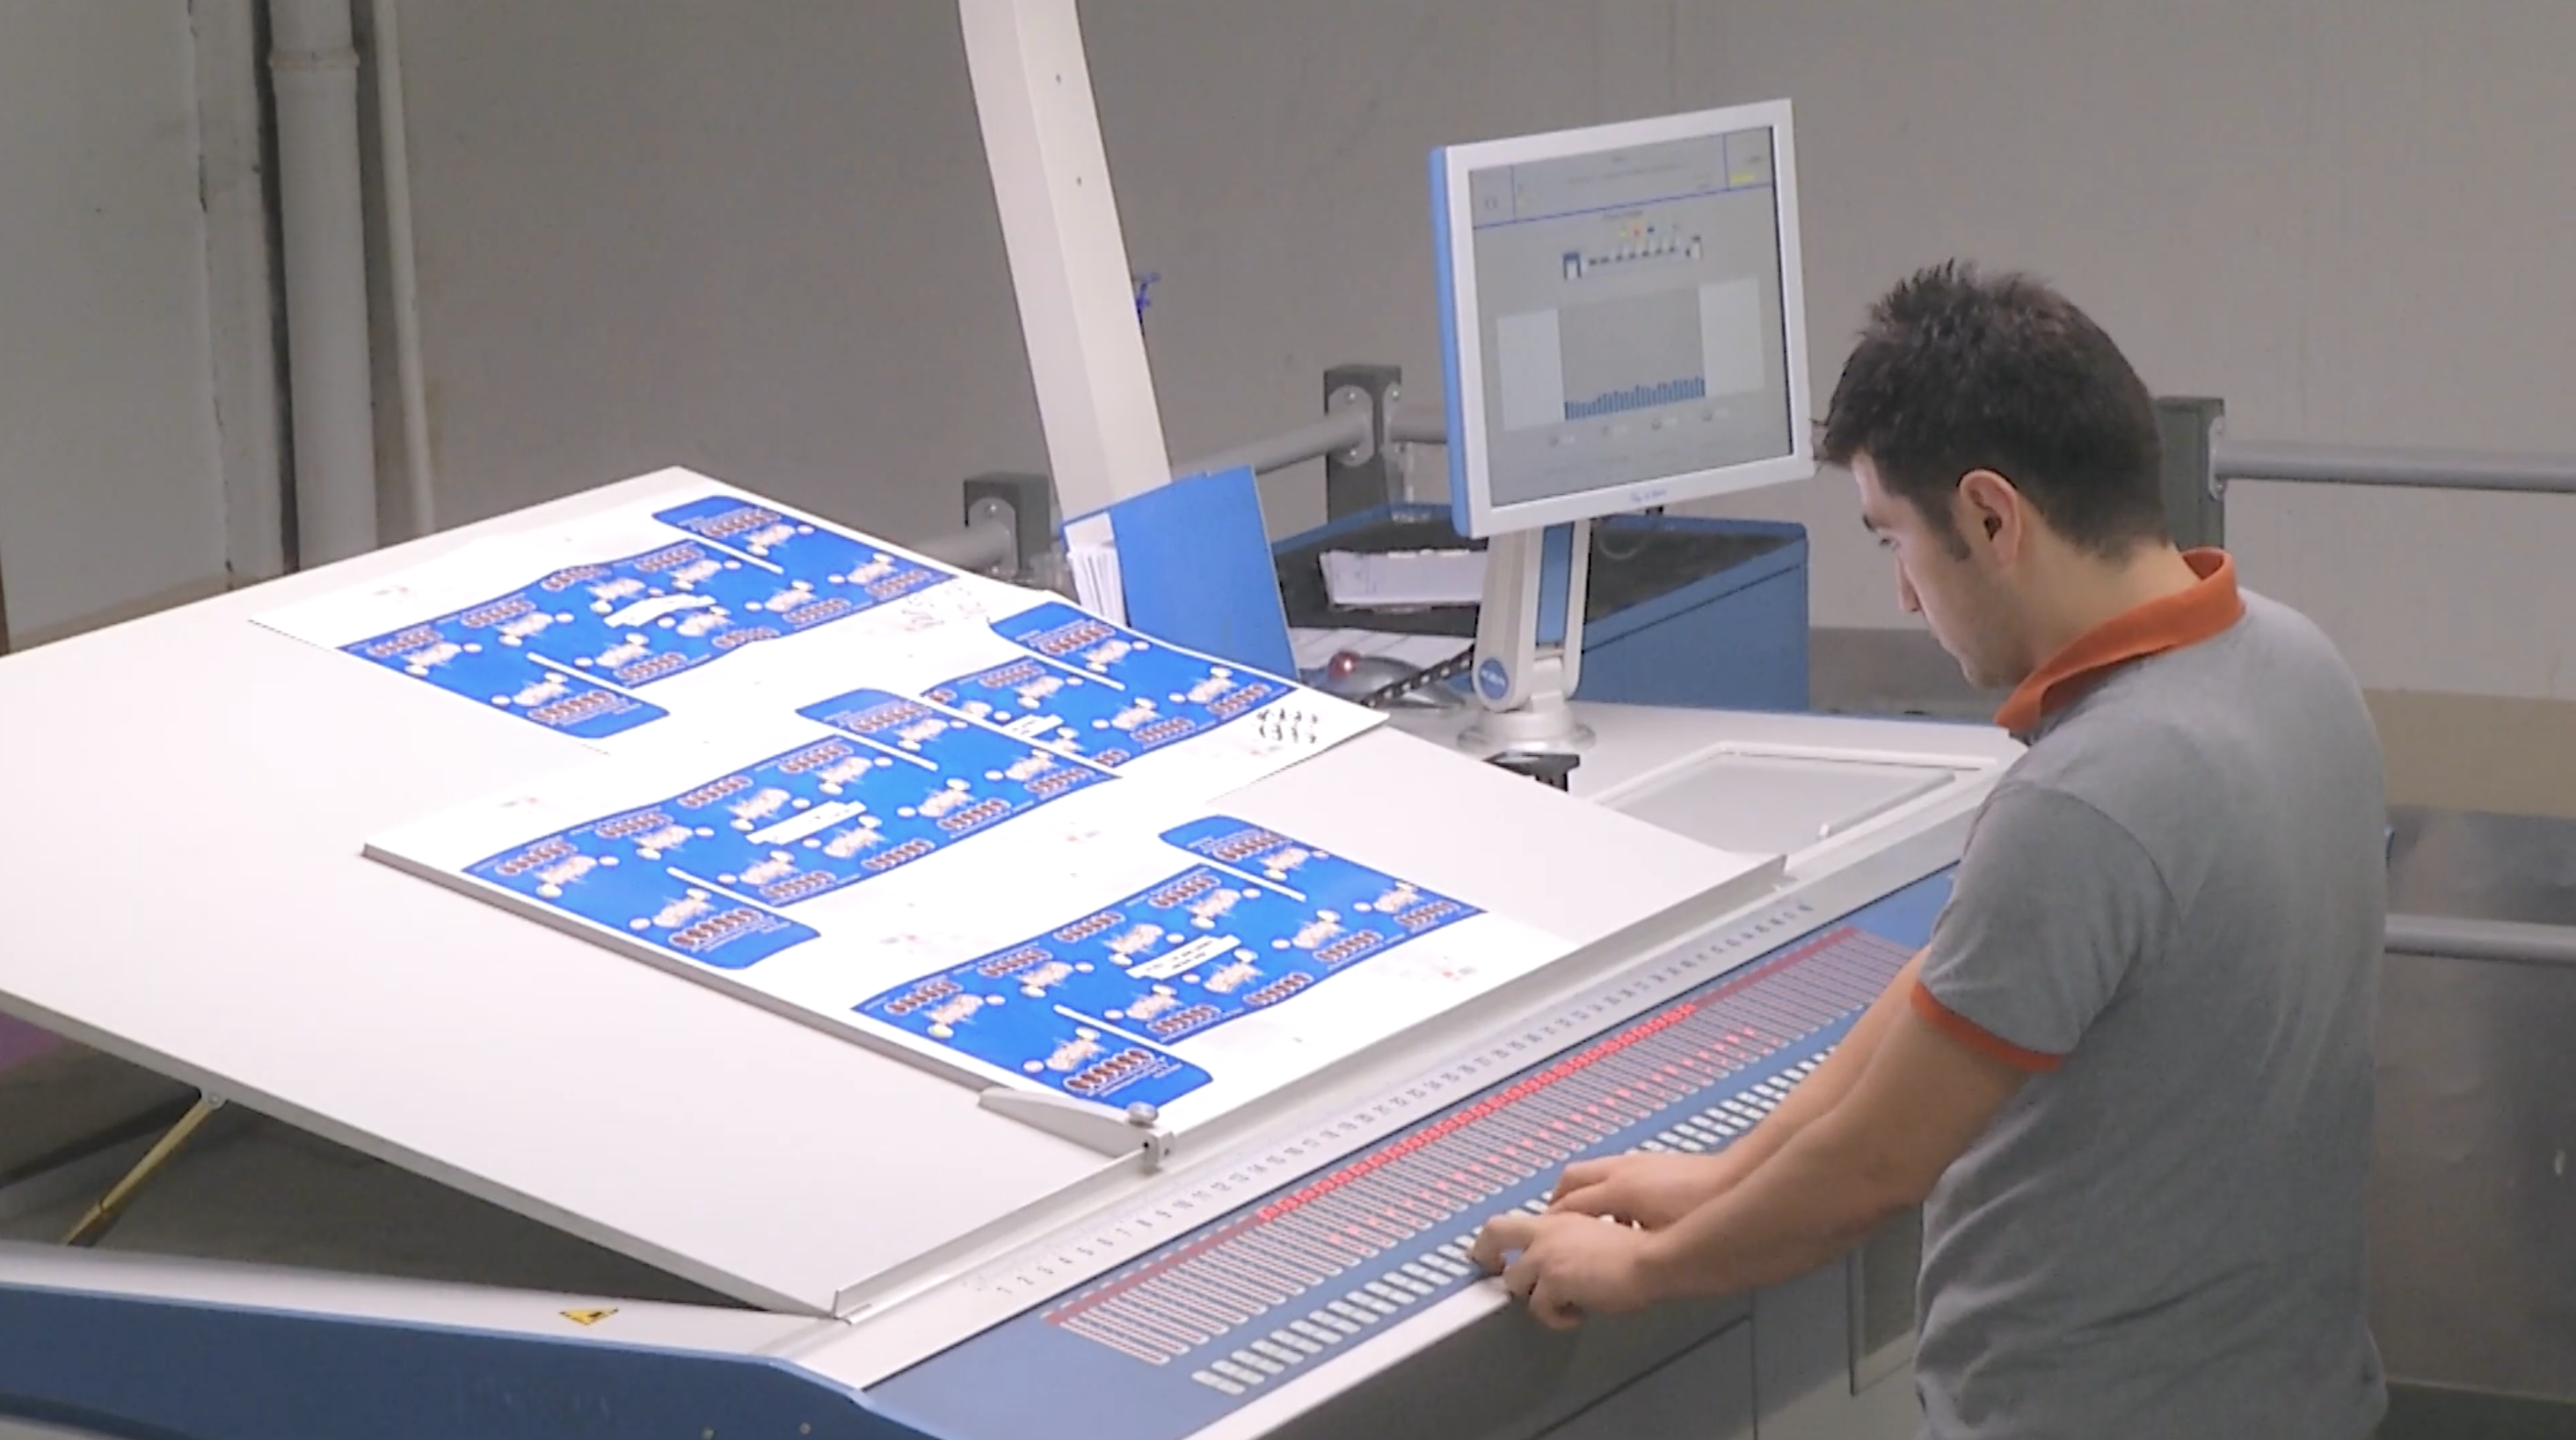
Instant color and technical control is provided with in-line spectrophotometers on each production line.
Final Approval
Each pallet undergoes a final check according to customer-specific specifications before shipment.
LABORATORY CAPABILITIES
Color Spectroscopy
We manage colors with ΔE < 2 precision using X-Rite technology.
Physical Tests
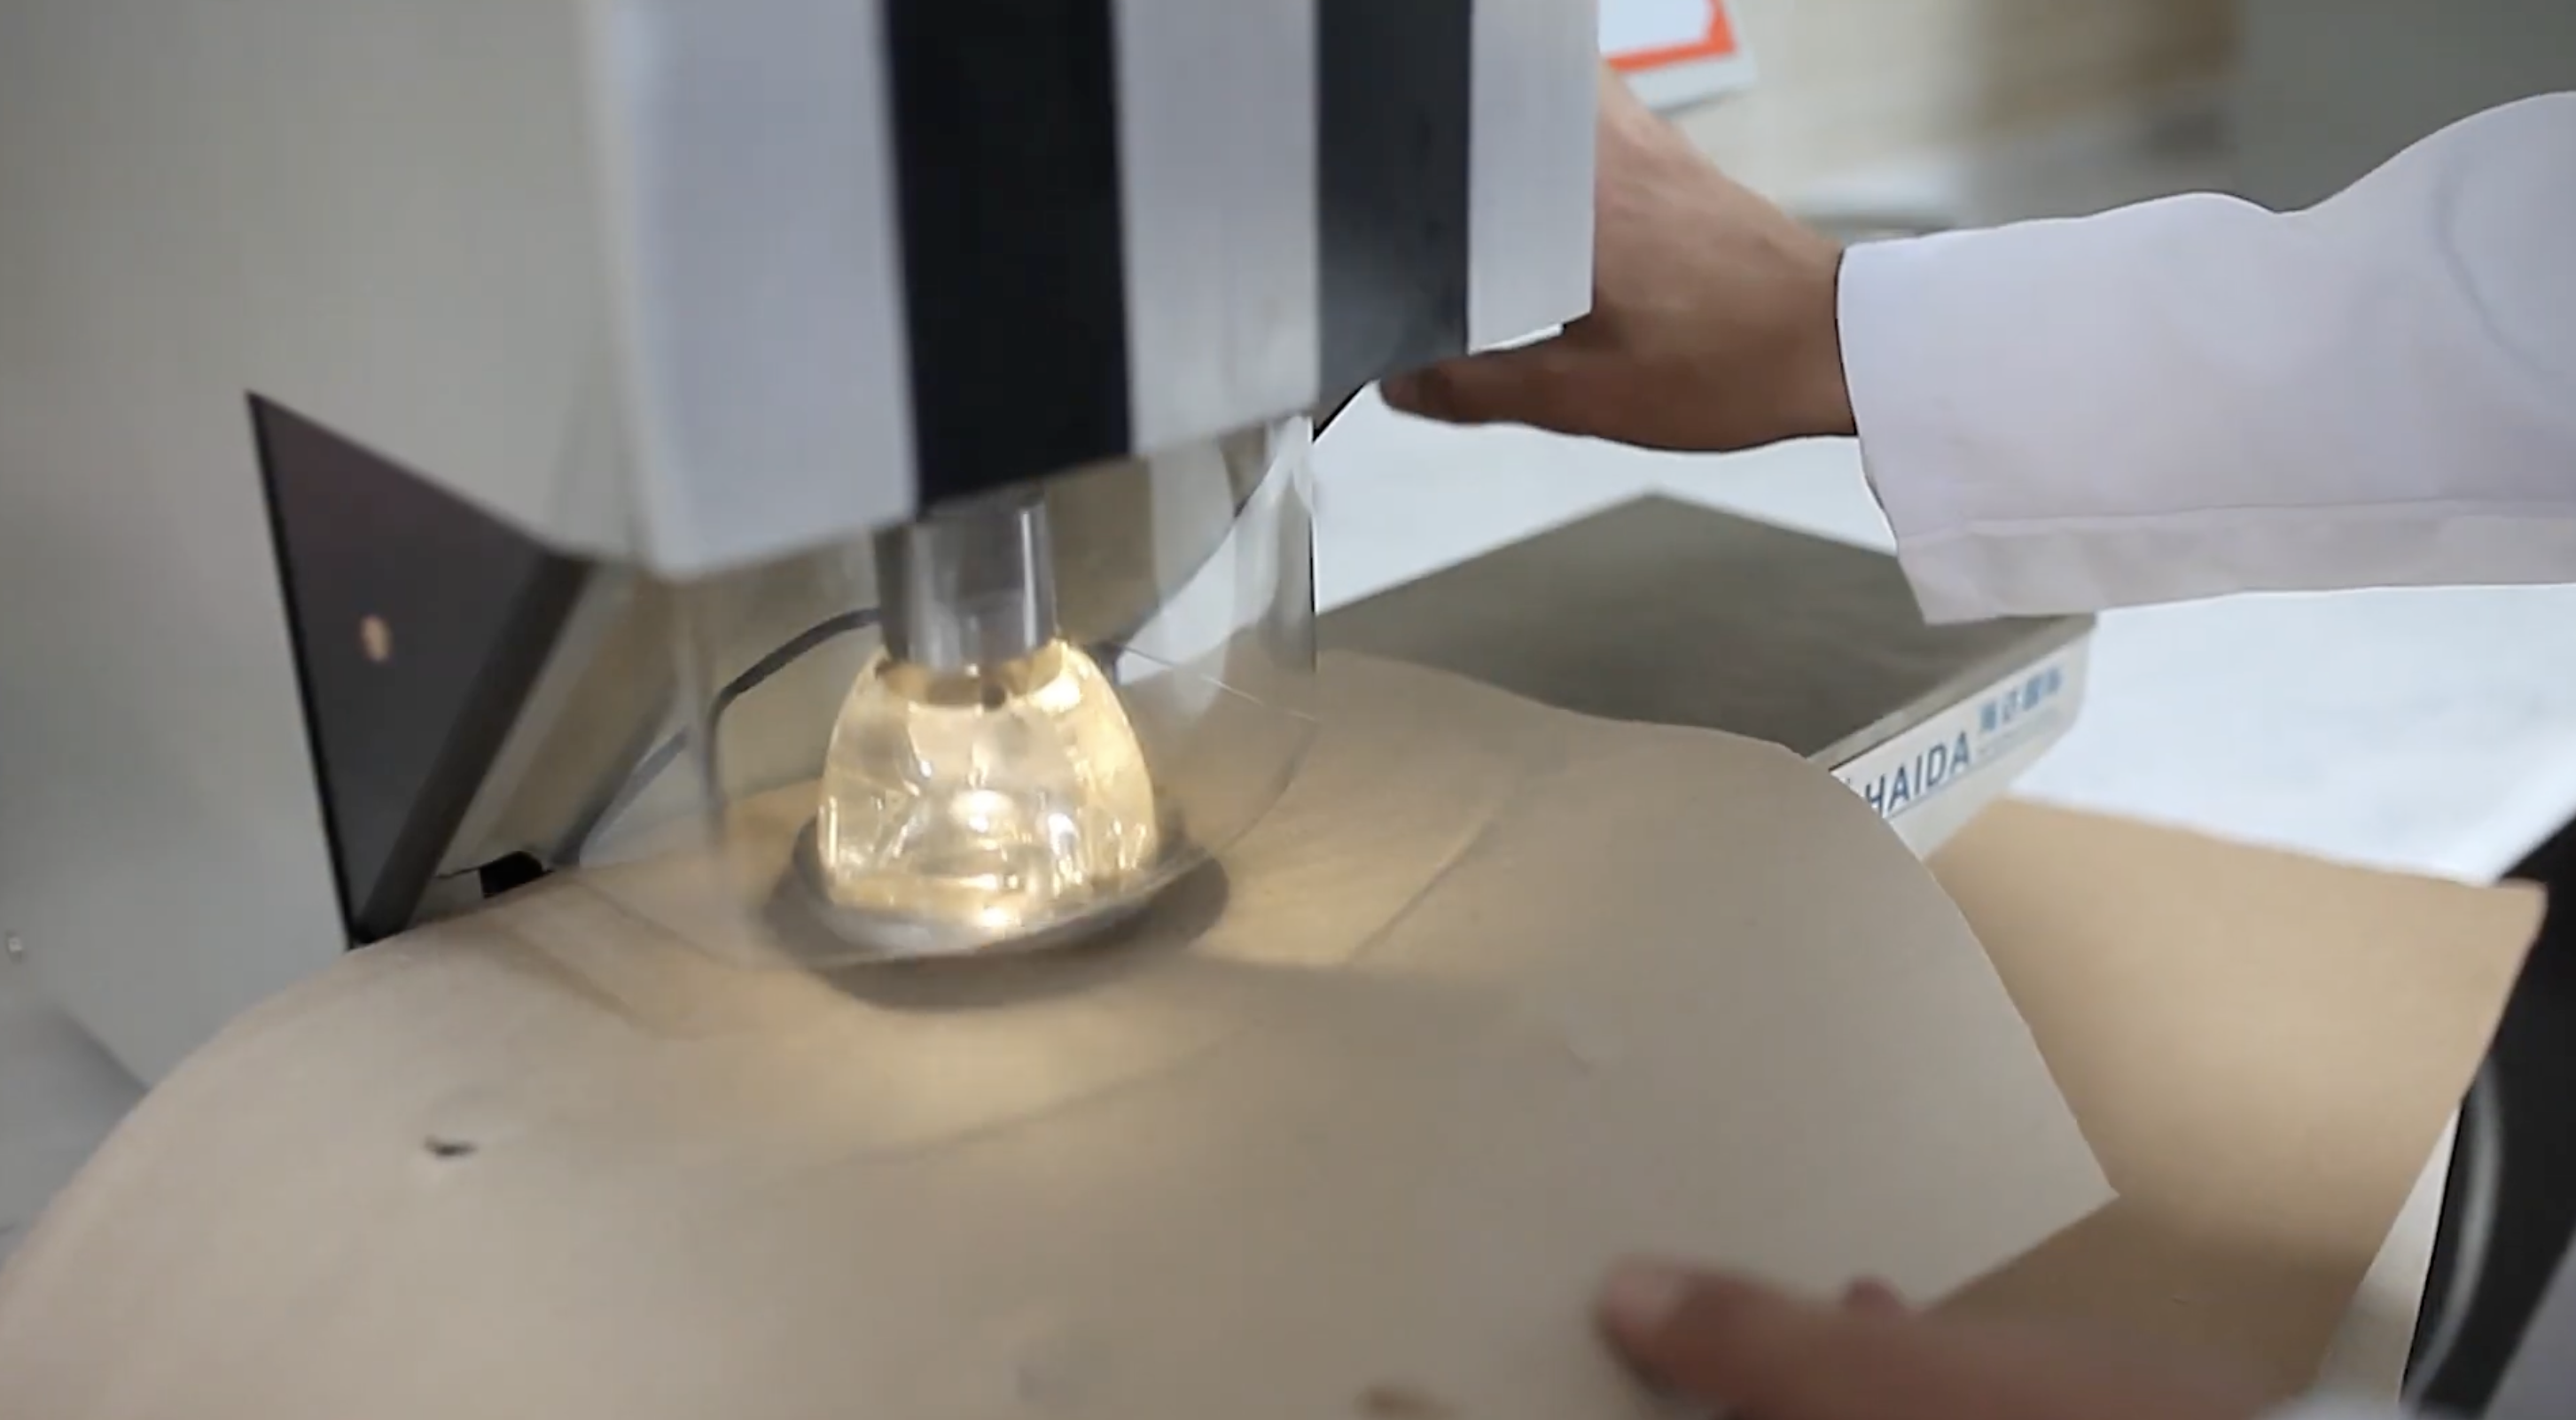
Burst resistance, moisture, and thickness tests are standard in every production.
- Migration Analysis
- Odor and Taste Tests (Robinson)
- Barcode Verification Tests
Uluslararası Sertifikalar
Certificates
"Look for our FSC®-certified products."